In contemporary exhibition architecture at the Saigon Exhibition and Convention Center (SECC, District 7), intricate metal facades, parametric partition screens, illuminated 3D corporate logos, and ultra-slender display frames have become indispensable design signatures. Handcrafted sheet metal fabrication can no longer meet the stringent tolerances, edge finishes, and lightning-fast turnaround times demanded by international exhibitors. Operating our 1,000 m² workshop in Nha Be equipped with advanced CNC machinery, Tin Long has industrialized architectural metalwork into a high-precision, turnkey process. Below is our manufacturing engineering breakdown.

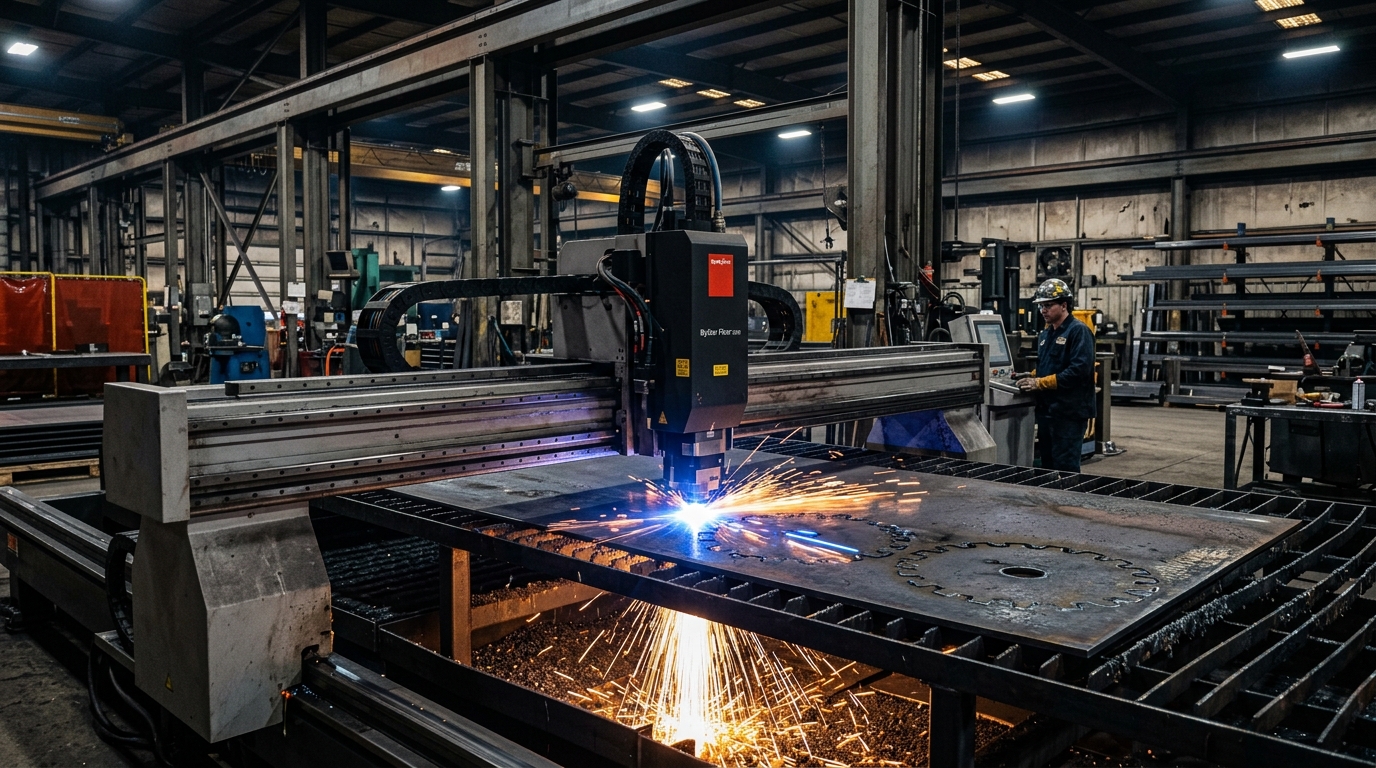
Figure 1: 6kW CNC Fiber Laser cutting machine processing high-precision architectural panels at the Nha Be plant.
1. 6kW CNC Fiber Laser Cutting & 3D Rotary Tube Cutting
Modern architectural metalwork requires cutting complex curves, micro-perforations, and interlocking mortise-and-tenon joints across diverse metals including carbon steel, stainless steel (SUS 304/316), and aluminum alloys.
1.1. Sheet Metal Laser Processing with High-Purity Nitrogen Assist
Tin Long operates high-power 6kW CNC Fiber Laser systems featuring autofocus cutting heads and intelligent nesting software. When cutting stainless steel and aluminum, high-purity Nitrogen (N2) assist gas at 16 to 20 bar pressure is utilized, preventing oxidation and delivering mirror-smooth, dross-free edge faces that require zero post-grinding before powder coating or plating.
1.2. 3D Rotary Tube Laser Cutting for Structural Frames
Fabricating modular exhibition frames traditionally required manual sawing, drilling, and grinding. With our 3D CNC rotary laser tube cutter, round pipes (Ø20mm to Ø220mm) and square tubes (up to 150x150mm) are cut with mortise slots, miter angles, and interlocking tabs in a single automated pass. Assemblers simply click components together on the SECC floor with zero measurement ambiguity.
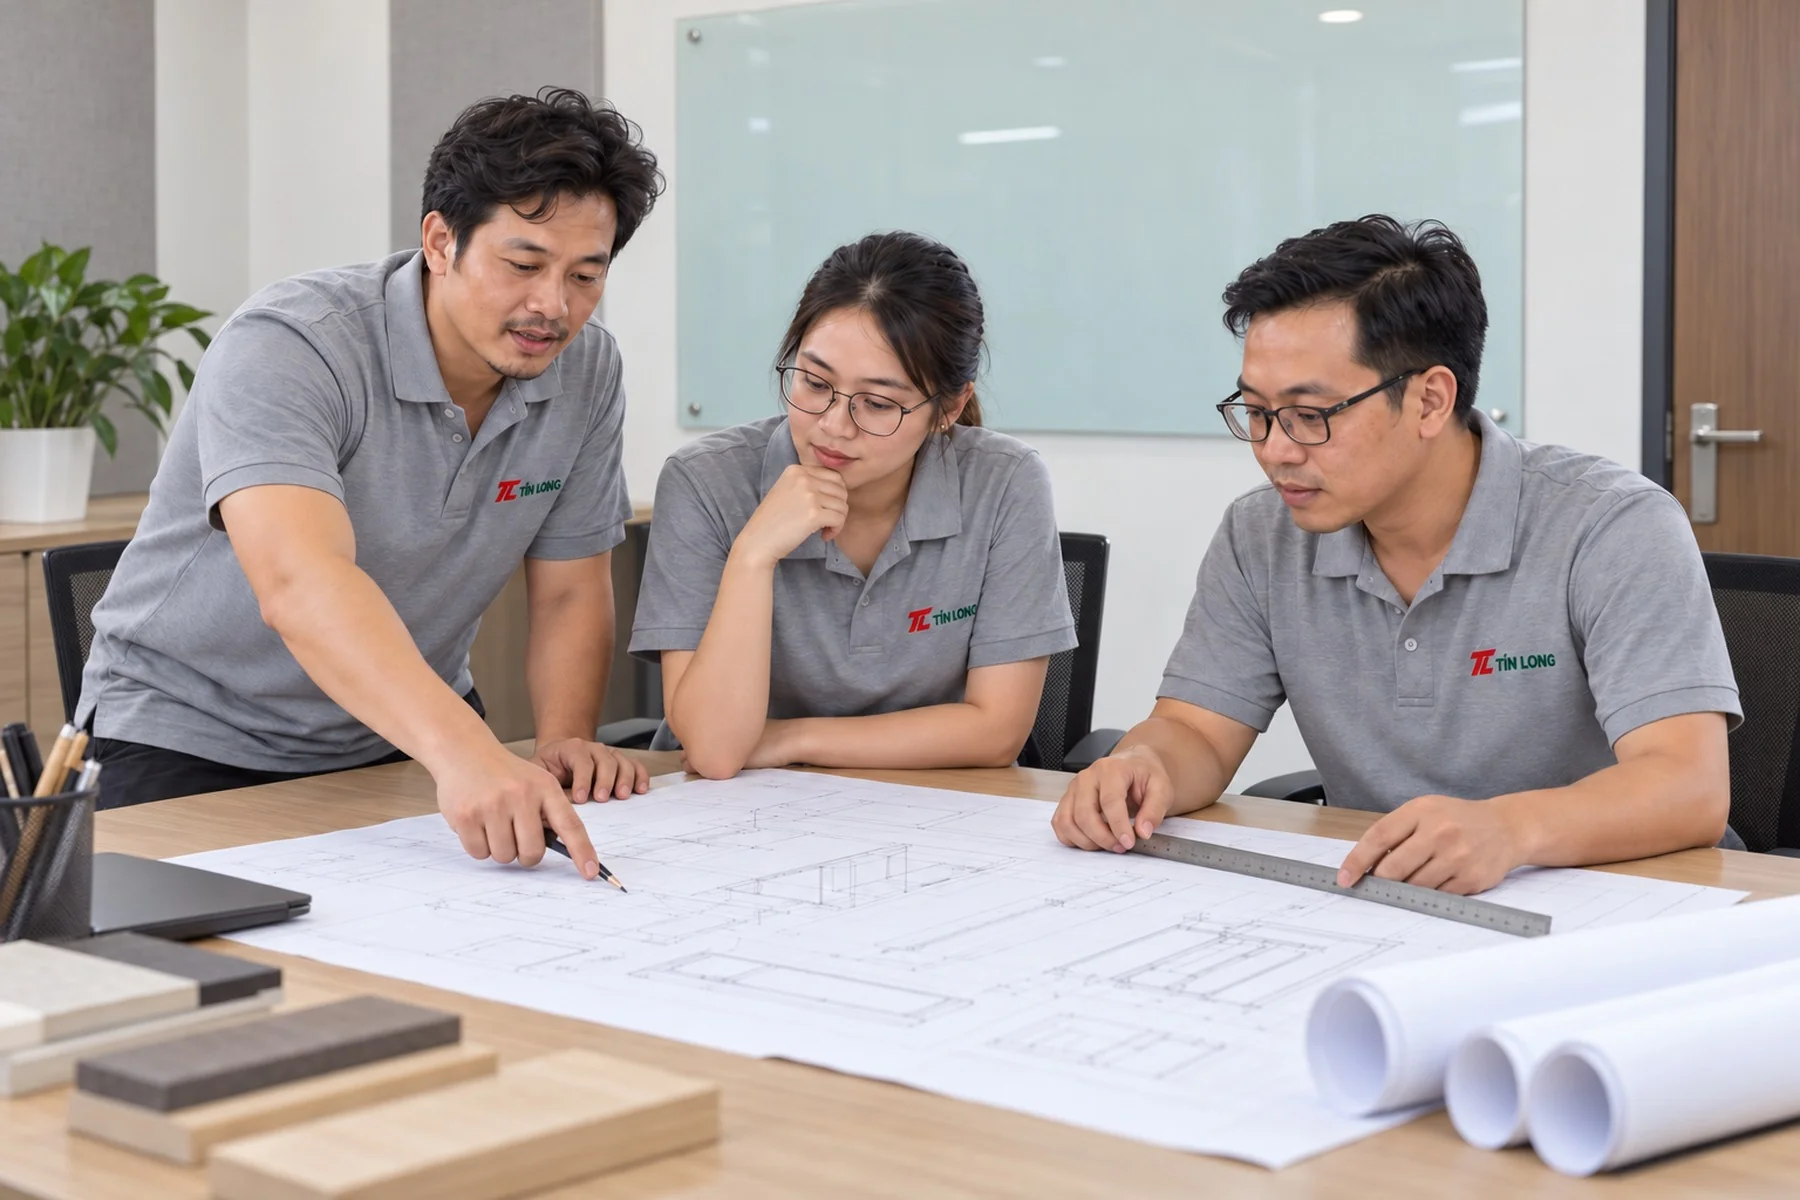
Figure 2: CAM software nesting optimization to maximize raw material yield and achieve ±0.05mm part repeatability.
2. Multi-Axis CNC Press Brake Bending & Precision Forming
Accurate sheet metal bending is critical to ensuring display cabinets, canopy fascias, and partition pillars align without unsightly gap variations.
2.1. Synchronized Multi-Axis CNC Press Brakes
Tin Long utilizes 160-ton electro-hydraulic synchronized CNC press brakes with dynamic crowning compensation. Angle measurement sensors automatically correct for material springback across bends up to 3,200mm in length, holding bending angular tolerances within ±0.3°.
2.2. Scratch-Free Bending for Pre-Finished Materials
When forming brushed stainless steel or pre-anodized aluminum sheets, tooling is lined with polyurethane protective films and urethane die inserts, preventing tool marks and preserving pristine surface finishes.
| CNC Fabrication Process | Equipment Capacity | Workable Material Range | Achievable Tolerance |
|---|---|---|---|
| Fiber Laser Sheet Cutting | 6,000 Watt, bed 2,000 x 6,000mm | Steel 0.5 – 25mm, SUS 0.5 – 16mm, Al 0.5 – 12mm | ± 0.05 mm |
| 3D Tube Laser Cutting | 3,000 Watt rotary chuck, 6,500mm length | Round Ø20 – 220mm, Square 20x20 – 150x150mm | ± 0.10 mm |
| Multi-Axis CNC Bending | 160-Ton, 4+1 Axis, length 3,200mm | Sheet thickness up to 6.0mm mild steel | Angle ± 0.3°, flange ± 0.2mm |
| Fiber Laser Handheld Welding | 1,500 Watt continuous & pulsed | SUS 304, Mild Steel, Aluminum alloys | Minimal heat zone, zero weld distortion |
| Automated Powder Coating | Batch convection curing oven 7,000mm | Polyester, Epoxy, PVDF architectural coatings | Film thickness 60 – 90 microns |
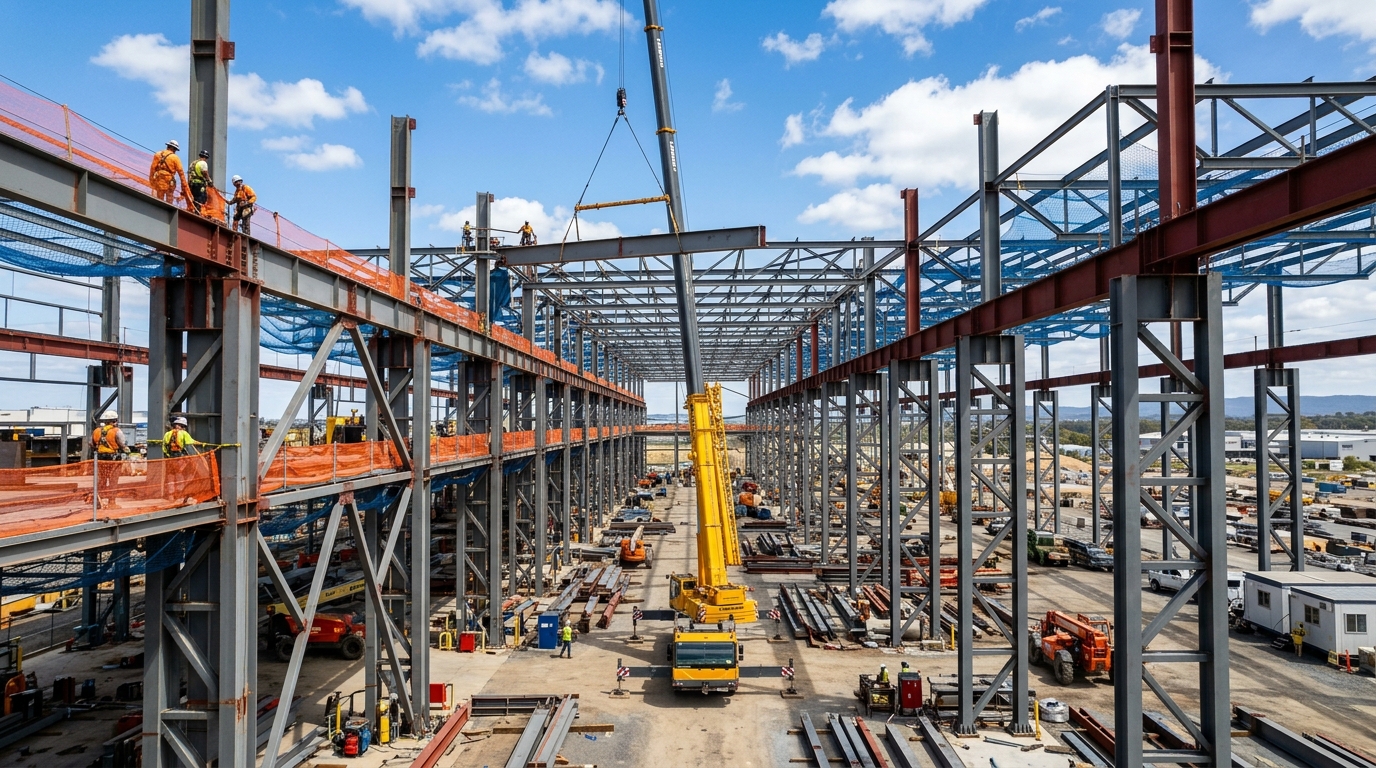
Figure 3: Prefabricated metal frameworks undergoing dimensional verification prior to surface coating.
3. Handheld Fiber Laser Welding & Fine Architectural Finishing
Traditional TIG and MIG welding inflict excessive localized heat, causing thin sheet metal (1.0mm – 2.0mm) to warp and discolor, requiring hours of tedious body-filling and sanding.
3.1. Ultra-Low Heat Input Fiber Laser Welding
Tin Long deploys 1.5kW handheld fiber laser welding systems. The ultra-narrow, high-energy laser beam achieves deep penetration with minimal heat-affected zones (HAZ). Thin stainless steel and aluminum panels are welded with virtually zero thermal distortion and smooth bead profiles.
3.2. Automated Electrostatic Powder Coating & Surface Treatments
All finished metal elements undergo a 7-stage chemical pre-treatment (degreasing, rust removal, and nano-zirconium conversion coating) prior to applying architectural polyester powder coatings cured at 200°C. Coatings exhibit 4H pencil hardness, exceptional impact resistance, and vibrant matte, satin, or textured visual finishes.
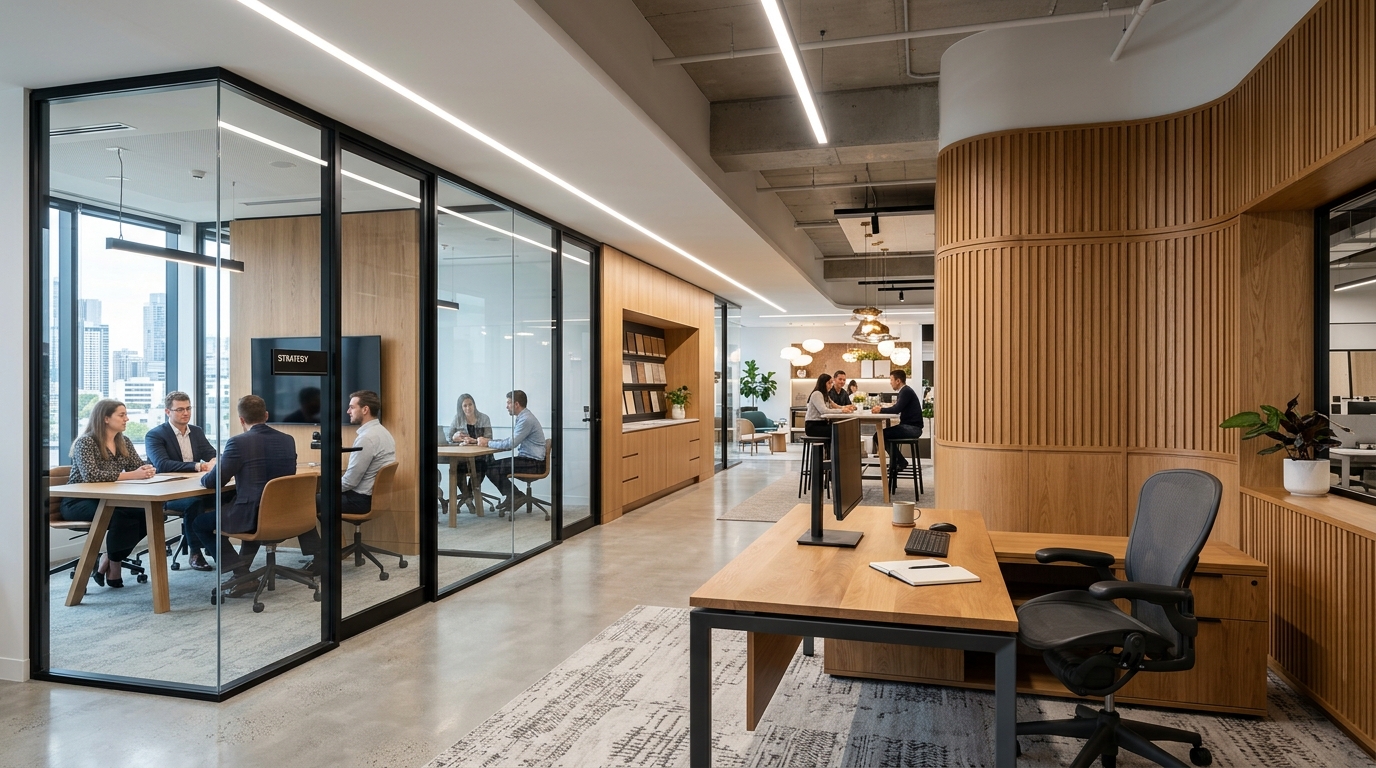
Figure 4: Seamless architectural result: Laser-cut decorative metal panels with embedded backlight illumination at SECC.
4. Modular Pre-Engineering for Rapid SECC Turnaround
On-site hot-works and welding are strictly prohibited inside SECC exhibition halls. All metal systems fabricated by Tin Long are engineered with mechanical interlocking hardware for silent, clean assembly.
4.1. Interlocking Tabs & Blind Fasteners
Decorative screens and wall claddings are fitted with CNC laser-cut keyhole slots and blind studs, allowing large partition sections to hang securely on structural frames without visible hardware.
4.2. Factory Trial Assembly & Protective Packaging
Every complex metal feature is erected in a 100% trial assembly at our Nha Be plant to verify joints and illumination before being wrapped in protective foam and delivered to SECC.
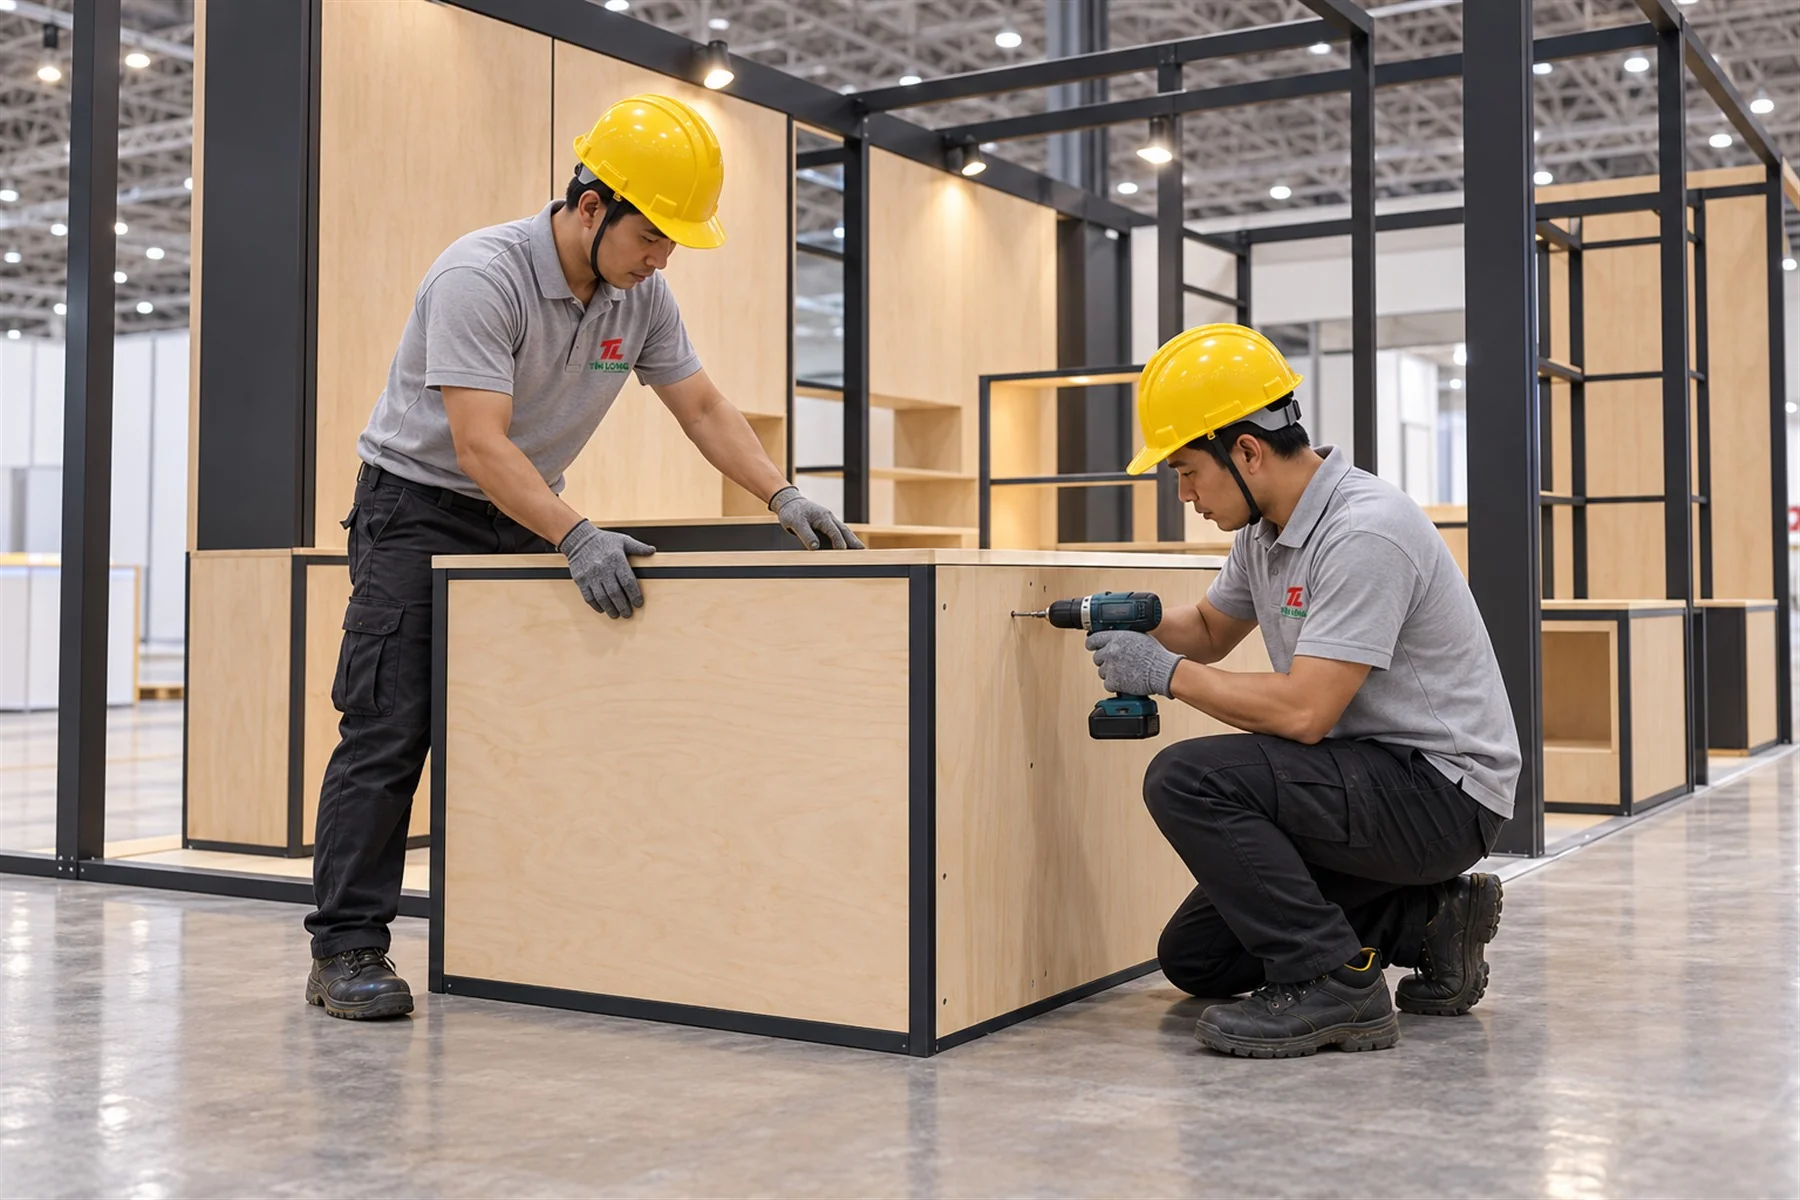
Figure 5: Clean, swift modular installation on the SECC exhibition floor with zero hot-works.
5. Precision Manufacturing from Tin Long
Bridging creative architectural design with high-technology precision metalworking is Tin Long's core competitive edge. Backed by our 1,000 m² workshop, CNC fiber lasers, and experienced engineering craftsmen, we transform the most ambitious metalwork concepts into stunning, flawless reality at SECC District 7.